

Wood Chipper Blades: Replacement Fit and Buying Guide
Release time: 2026-10-28
For a used knife, record its present dimensions separately from the original specification. Sharpening changes the working edge, and a replacement copied from that edge may reproduce the wear. Resolve the original geometry before releasing a manufacturing drawing.
Have a drawing or an old knife? Send NJDETE the machine identity, part details and required quantity for a drawing-based replacement enquiry.
Replacement specification at a glance
This guide covers purchasing replacement chipper knives for a defined disc or drum machine. It also covers the information needed to assess a used knife before ordering. It does not establish a common knife size or setup for every chipper.
| Specification item | Establish before comparing offers |
|---|---|
| Machine and part identity | Manufacturer, model, serial range, knife position and current part number |
| Finished geometry | Approved drawing revision, dimensions with units, bevel and mounting references |
| Installation interface | Seating face, holes or slots, clamping arrangement and applicable hardware specification |
| Material and condition | Approved steel and heat treatment, required verification and any proposed change |
| Supply scope | Quantity for each part, the machine’s matched-set requirements and separately included components |
Identify the knife and the cutting assembly
Chipper knives cut wood in a rotating disc or drum arrangement. The assembly can include a stationary counter-knife or anvil, a holder and a clamping system. Establish which component is being ordered. A rotor knife, counter-knife and clamp bar may be related parts, but they need separate identities and order quantities.
A disc or drum description narrows the machine family; it does not define the replacement. Two machines described as drum chippers can use different knife lengths, mounting details or working positions. Even an unchanged model name may cover a serial-number revision or a modified holder.
Start with the machine’s parts documentation and current approved drawing. Add photographs of the installed position when they can be obtained under the prescribed maintenance procedure. Knife removal and measurement belong with qualified personnel using the machine’s isolation and rotor-restraint procedure.
For customers choosing a machine rather than a replacement part, the industrial knives guide compares knife categories by cutting task and mounting arrangement. Keep a hooked shredder cutter and a straight chipper knife on separate enquiry lines.
Describe the wood that actually reaches the knife
State whether the machine handles logs, branches, sawmill offcuts or another approved feed. Include the species where known, moisture condition, bark content, maximum section and the presence of soil, stones or metal. Clean wood and contaminated recovered wood are different purchasing discussions.
If you want a material change, explain the observed problem. Gradual edge rounding, a local chip after a foreign-object event and recurring damage at one mounting position call for different investigations. Photographs and a feed record are more useful than a request for the hardest available steel.
Measure from references that survive wear
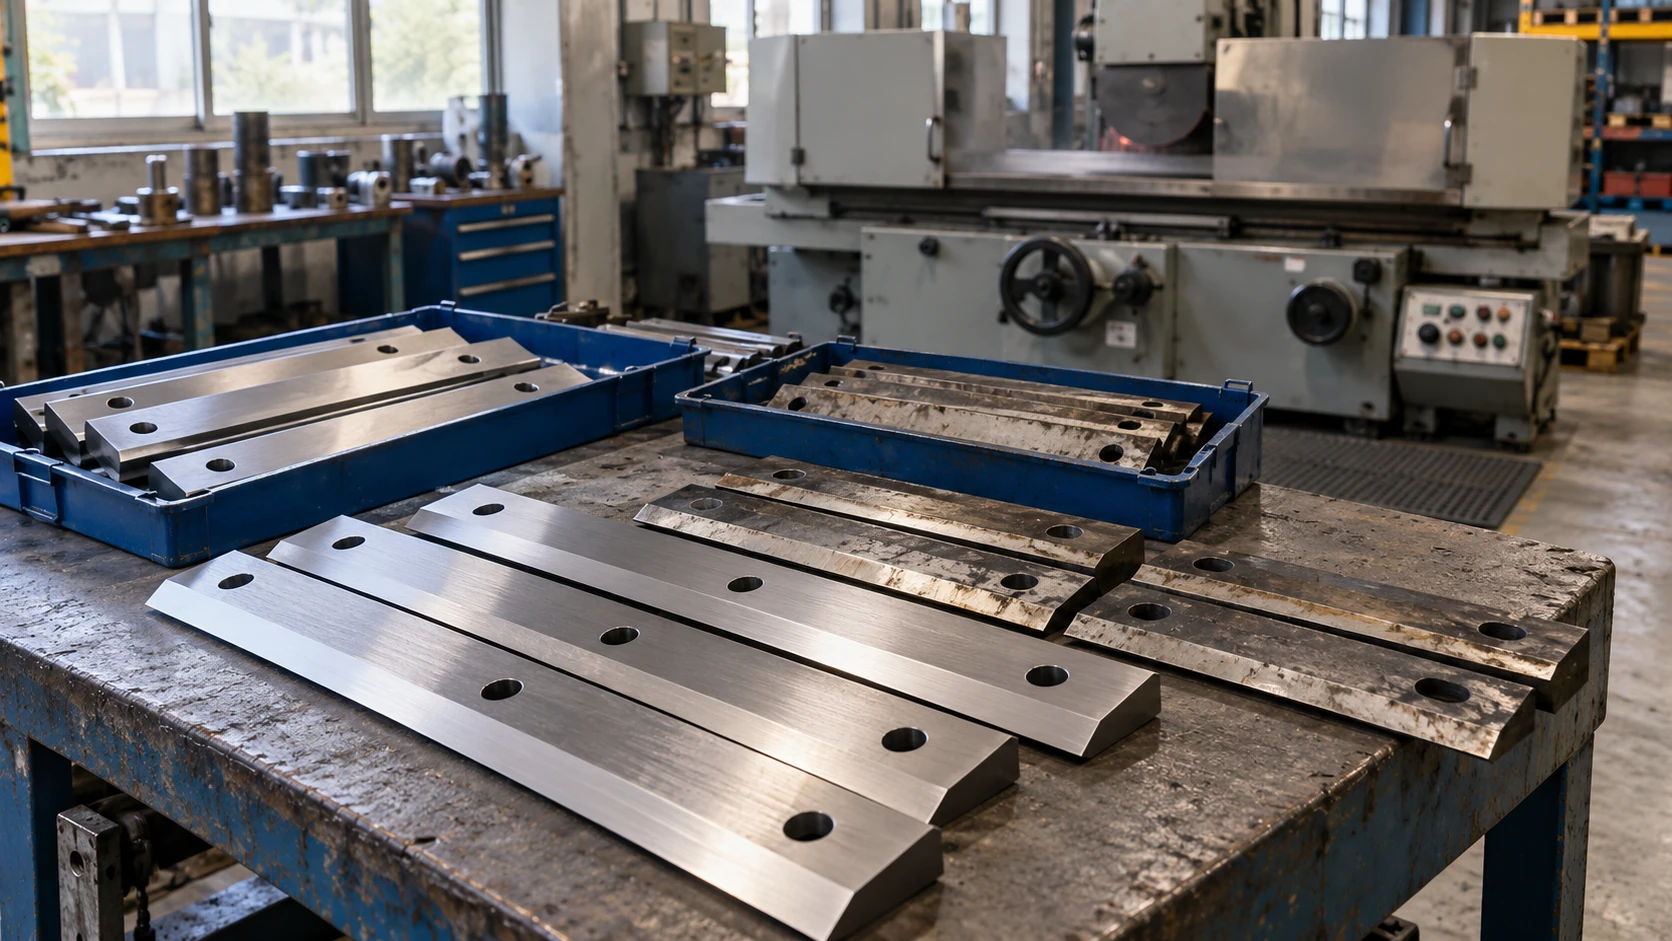
Use a drawing that locates the cutting edge from the mounting and seating features. Agree on the reference end and back face before recording hole coordinates. This prevents one supplier measuring from an unworn back edge while another works from a shortened cutting edge.
| مقال مميز | Information to record | Purchasing mistake it helps prevent |
|---|---|---|
| Overall envelope | Length L, width W, thickness T and units | Ordering a similar outline in the wrong size or unit system |
| Mounting pattern | Hole or slot type, count, size and coordinates from named references | Assuming equal hole count means equal fit |
| Cutting edge | Bevel face, edge profile and edge position relative to mounting references | Reversing the bevel or copying a worn edge location |
| Seating and clamping | Locating face, reliefs, steps and the relevant holder detail | A knife that fastens but does not seat as intended |
| Working limits | Approved service dimensions, adjustment limits and set requirements | Treating the smallest used sample as the new-part specification |
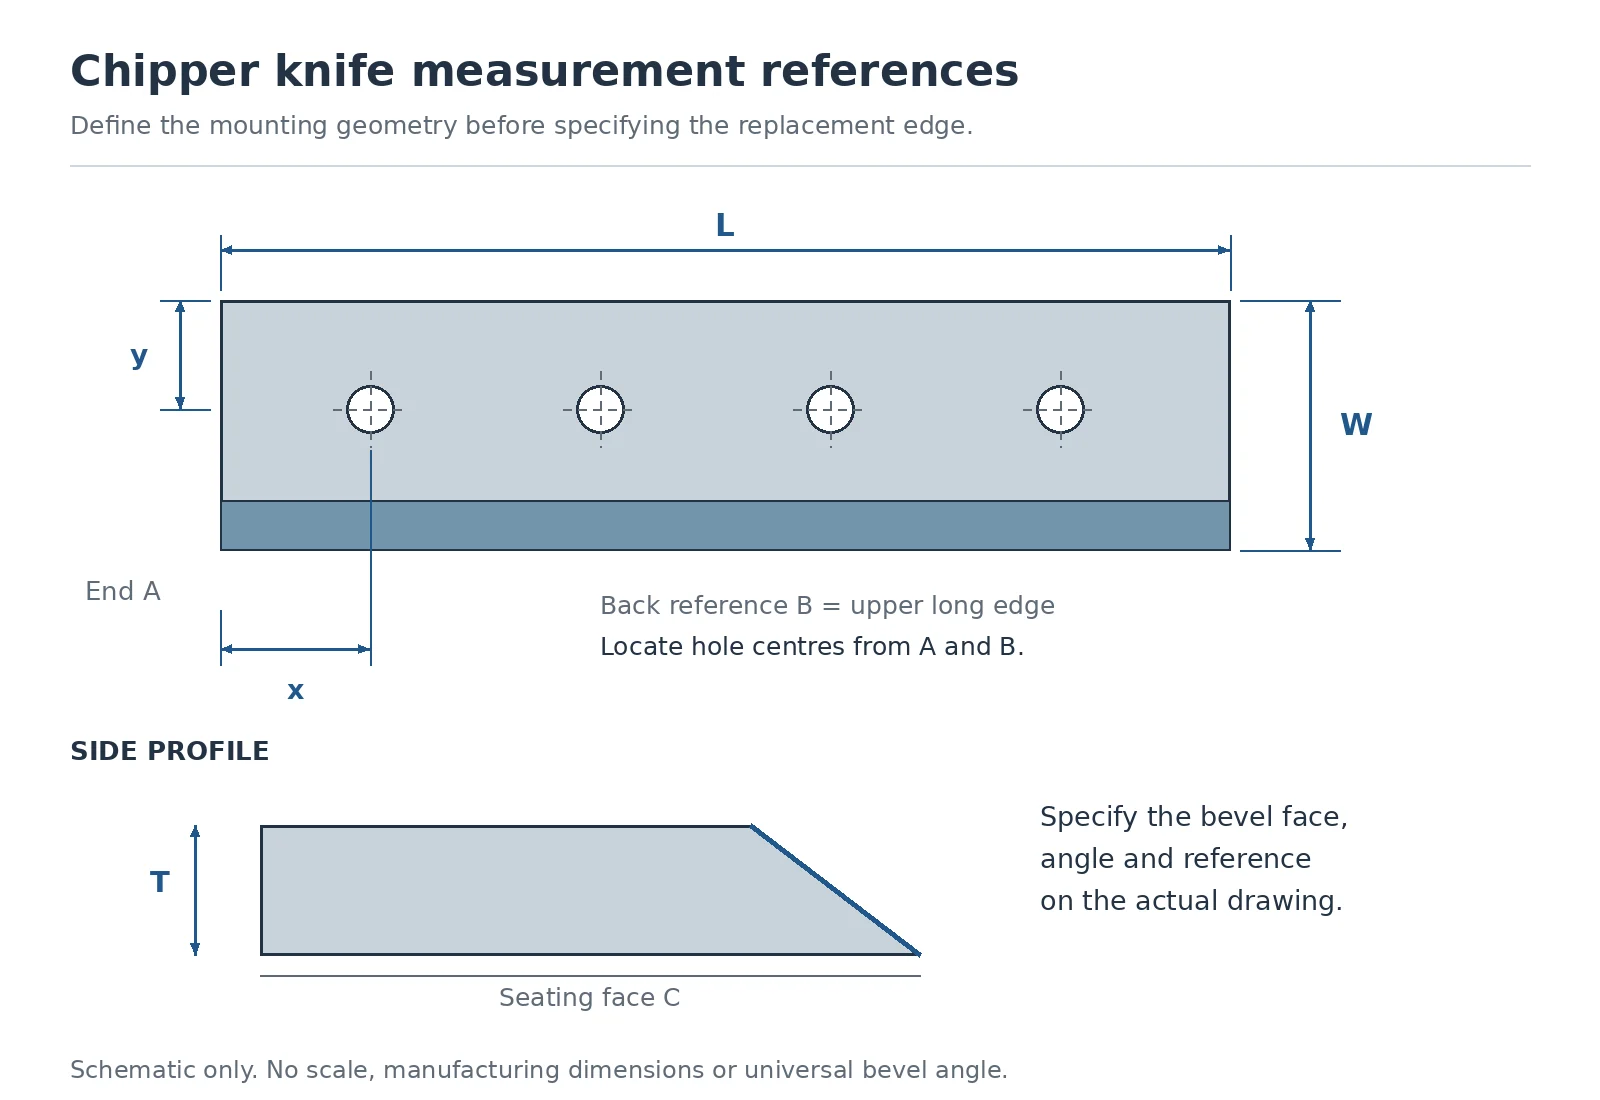
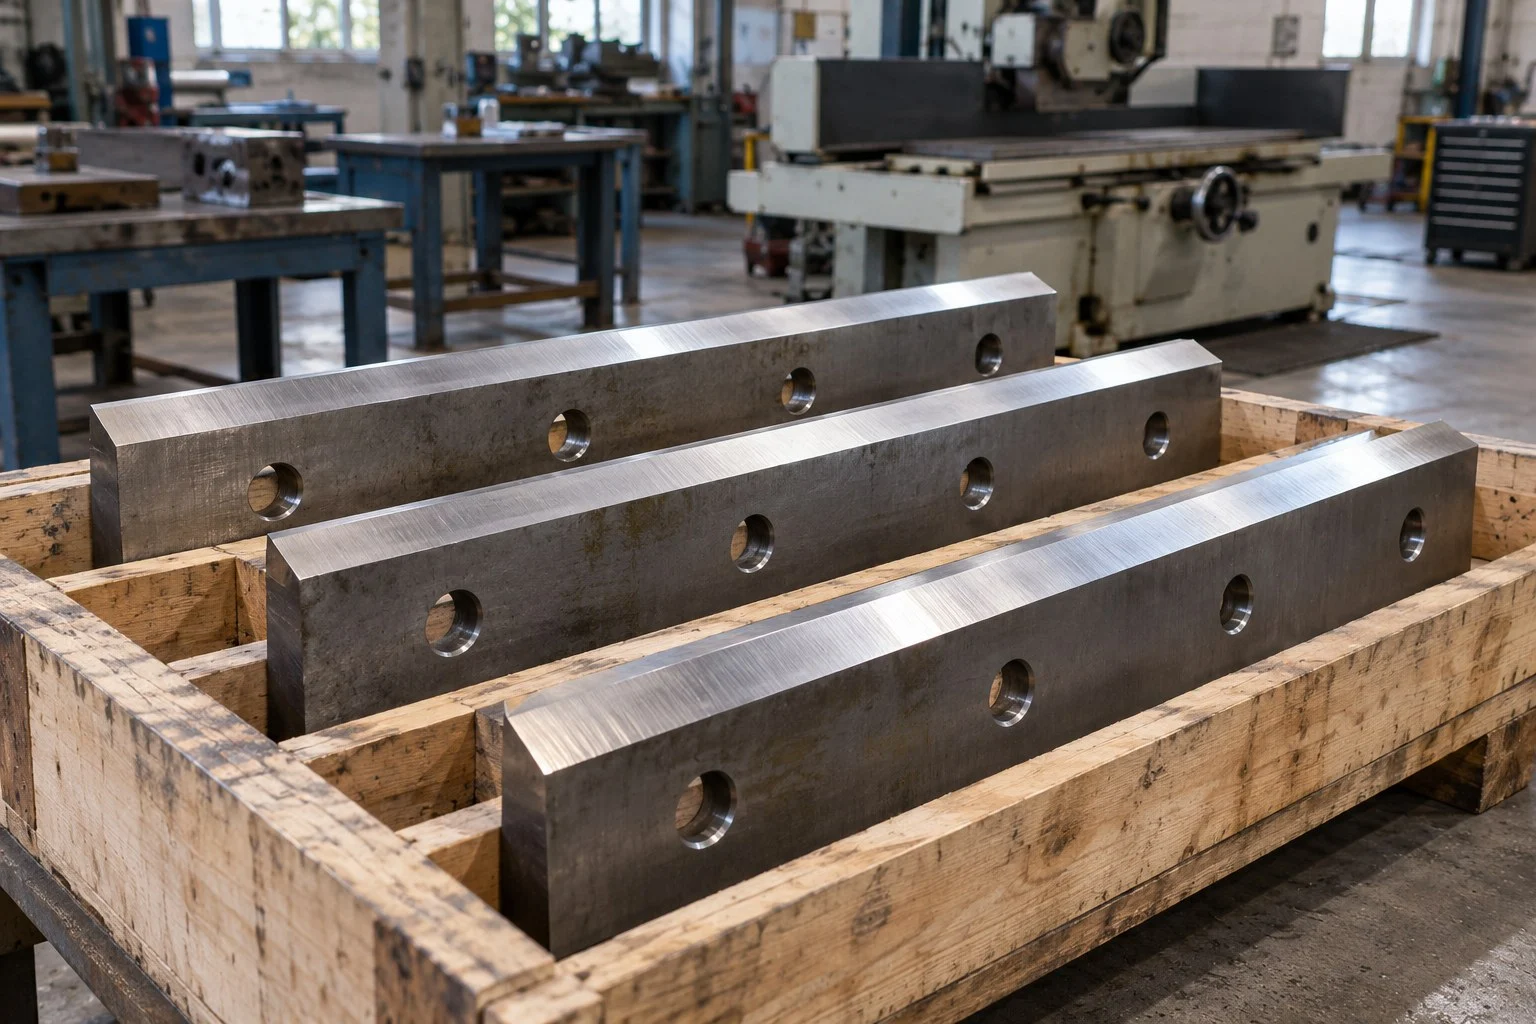
Record countersinks, counterbores and threaded features explicitly. A photograph looking straight down can hide those differences. Include both faces, the end or side profile and a close view of each unusual mounting feature.
If only a used sample is available, label measured values as current sample dimensions. Keep earlier drawings, invoices and sharpening records with it. Ask the technical reviewer to resolve missing original dimensions rather than extrapolating them from a scaled photo.
A useful dimensional check before releasing the drawing
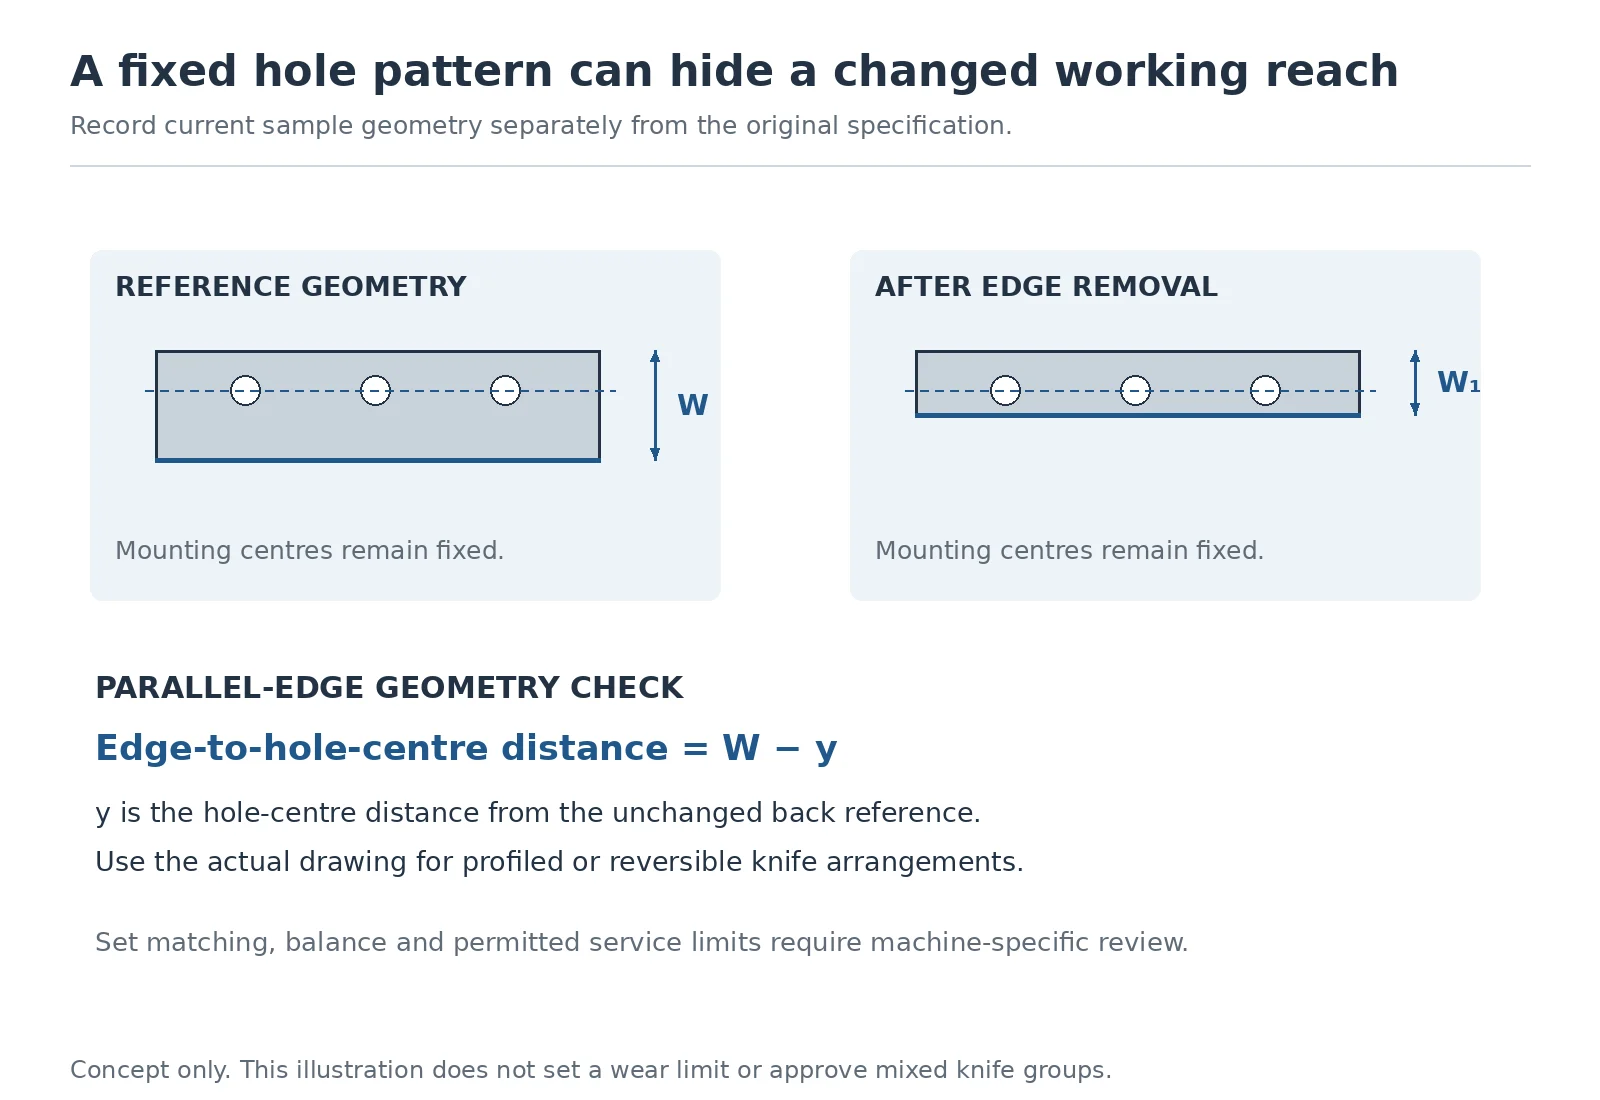
For a simple knife with parallel back and cutting edges, a hole centre at distance y from the back reference and an edge at width W gives an edge-to-hole-centre distance of W − y. Grinding that edge reduces this distance when the mounting feature stays fixed.
That relationship explains why an unchanged hole pattern can coexist with a different working reach. It is a geometry check, not a remaining-life calculation. Use the actual drawing for profiled or reversible knives, and obtain the machine’s permitted limits before judging serviceability.
Decide whether to assess, sharpen or replace
An edge photograph helps describe condition. It cannot confirm remaining material integrity or suitability for continued use. Keep the observation separate from the proposed disposition.
| الحالة الملاحظة | Information needed for review | Decision to resolve |
|---|---|---|
| Progressive dulling with no reported impact | Service history, current geometry and applicable regrinding limits | Whether an approved service can restore the required geometry |
| Local edge loss after a suspected contaminant | Damage location, feed event and inspection findings | Cause, extent of damage and whether replacement is required |
| Suspected crack or damaged mounting feature | Identification, photographs and qualified inspection | Hold for an authorized disposition before reuse |
| Poor chips after fitting sharp knives | Setup record, mating-part condition and comparable feed description | Whether the problem lies elsewhere in the assembly or process |
Wood chipper blade sharpening removes material. Before authorizing it, confirm the required profile, minimum permitted dimensions and finished set requirements for the actual machine. There is no universal number of sharpening cycles that establishes acceptance.
Specify controlled grinding and post-service inspection through the responsible service provider. Do not turn a general angle found online into the specification for your part. If an edge cannot be restored within the approved limits, order a replacement to the correct new-part geometry.
Review the knife group, holder and mating part
Confirm which knives must be managed together. The machine documentation should define any pairing, dimensional matching or balance requirements. A single damaged knife is a reason to review the group; it is not enough information to decide how many new knives to buy.
When preparing an order for wood chipper replacement blades, list each knife position and retained component. Record the finished condition of retained knives and any permitted service arrangement. The technical reviewer must resolve whether the proposed combination is acceptable.
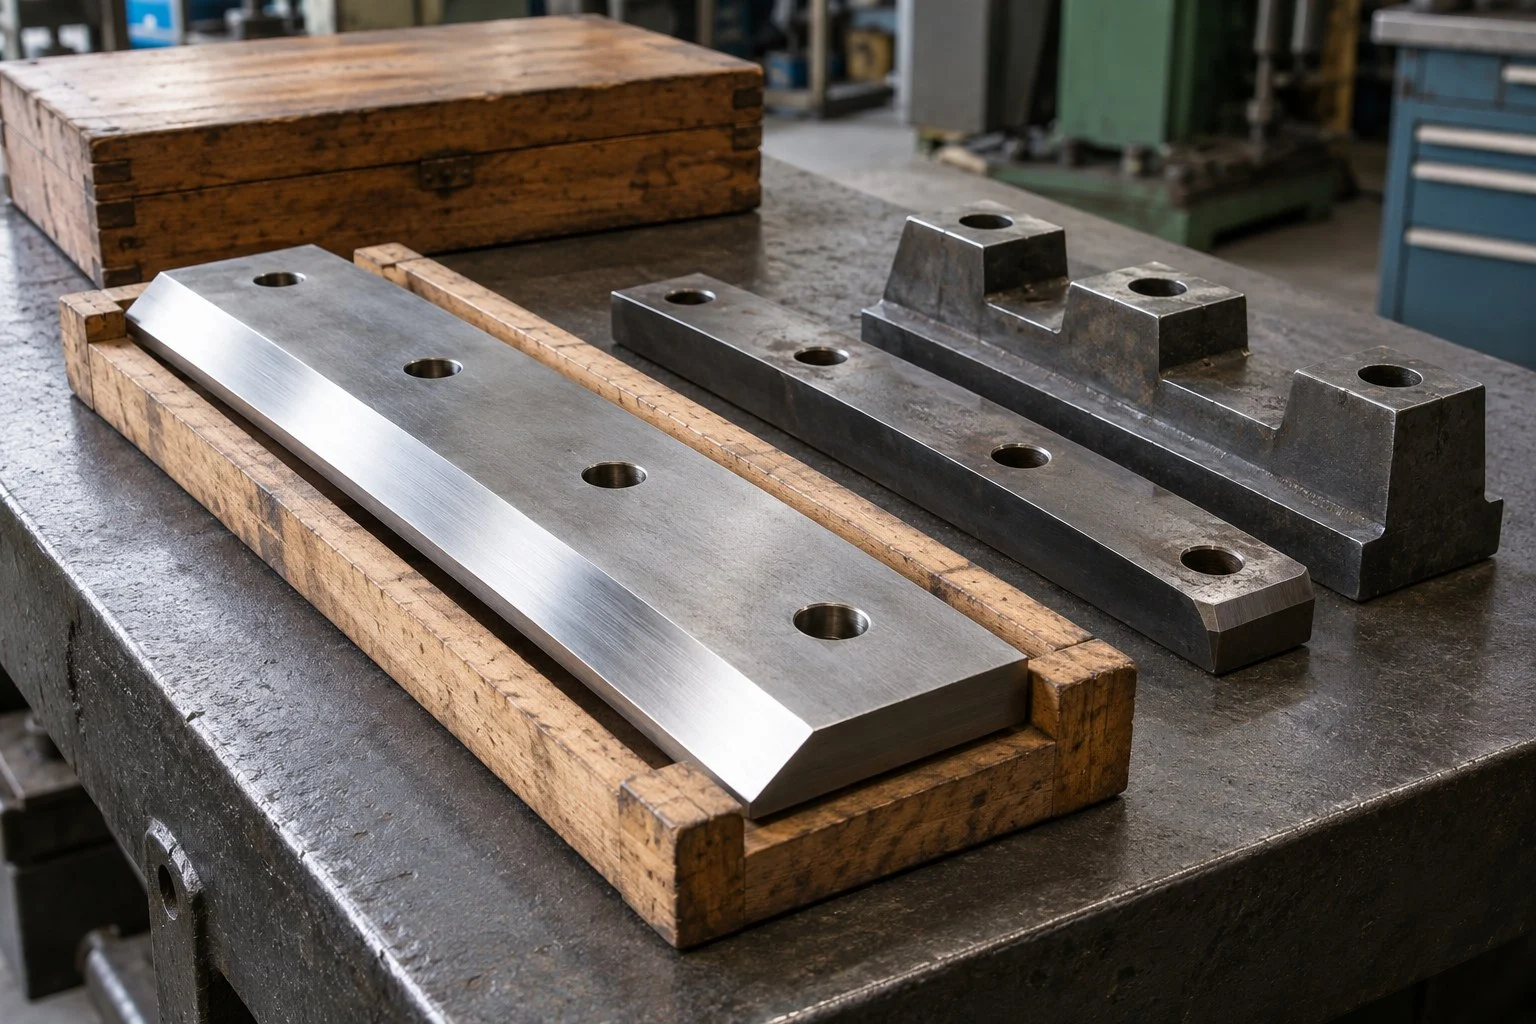
Inspect the holder and clamping interfaces through the machine’s maintenance procedure. If a seating surface is damaged or the counter-knife is worn, the purchase may require more than rotor knives. Identify the affected component instead of trying to compensate with an altered replacement blade.
Obtain the applicable requirements for fastener type, tightening, replacement and knife-to-counter-knife clearance. Keep those instructions with the job. Bolt diameter alone does not establish a tightening value, and a clearance from another model cannot close the specification.
Choose steel against a defined duty
Begin an exact replacement enquiry with the approved existing material and heat-treatment specification, where available. If that information is missing, say so. A trade description such as chipper steel is not a complete material specification.
For a proposed upgrade, describe the reason and the result to evaluate. Record the current knife condition, feed and operating context before changing the material. A comparison is difficult to interpret if the steel, bevel, feed and setup all change together.
| Requirement or problem | Evidence to put in the enquiry | What to agree with the supplier |
|---|---|---|
| Reproduce a working knife | Approved drawing, part identity and current material requirement | Exact specification and any declared substitution |
| Repeated wear in a known duty | Feed description, useful service interval and condition records | Proposed change and a comparable evaluation method |
| Chipping or abnormal breakage | Damage evidence and the event or operating history | Investigation and technical disposition before a material change |
| Verify a supplied knife | Purchase specification and required inspection scope | Material, heat-treatment and finished-part records appropriate to the order |
A hardness result is one item of evidence. It does not, by itself, identify the steel, establish toughness or predict operating life. Ask how a proposed material will be verified and which finished-part records accompany the order.
NJDETE’s company product overview includes chipper knives within its custom industrial knife range. Application-specific dimensions, steel, hardness, compatibility and inspection scope need confirmation for the proposed part. The custom straight and special-shaped blade guide explains how to prepare a drawing or sample for that discussion.
Compare replacement quotes on the same basis
An attractive unit price can leave out parts or inspection work needed for the job. Give suppliers the same drawing revision and request a separate line for each knife, mating part or hardware item. State which existing parts will remain in use.
| Quote item | Require a clear answer |
|---|---|
| Part identity and quantity | Which drawing revision, positions and quantities are included? |
| Material and geometry | Does the offer follow the specification, and are any changes proposed? |
| Group and assembly scope | Which knives form the required group, and which parts are retained or excluded? |
| Inspection and traceability | Which agreed measurements and material or process records will be supplied? |
| Delivery and discrepancy handling | What packaging, timing, delivery terms and nonconformity process apply? |
Keep knife purchase cost separate from service cost. If comparing cost per accepted tonne, use recorded costs and accepted output from comparable duty periods. State the currency, mass unit, feed, inspection basis and included costs. A lower price per knife does not establish a lower operating cost.
For repeat supply, retain the approved drawing, inspection requirements, order breakdown and change history. Use that package for the next enquiry instead of rebuilding the specification from workshop photographs.
Check the delivered parts before the operating evaluation
Confirm part identity, quantities and the agreed inspection records first. Have the designated technical reviewer assess geometry and the complete intended arrangement before release to service. Installation and commissioning follow the machine’s approved procedures.
Then record the operating evaluation separately: feed description, machine condition, elapsed operating time, accepted chip output, observed defects and the reason the run ended. Do not assign an improvement percentage to a new steel unless the comparison supports it.
Keep one replacement record for each job. Include the removed part’s identity and condition, the supplied drawing revision, inspection results, installation approval and subsequent observations. That record supports the next purchasing decision and helps distinguish an isolated feed event from a recurring problem.
Frequently asked questions
Are wood chipper blades universal?
No. Confirm the part number, serial applicability, drawing, mounting and complete working arrangement. Similar overall dimensions or a matching hole count do not establish compatibility.
What is the correct wood chipper blade angle?
Use the angle and its reference convention from the approved part drawing or the machine’s documentation. A number without the bevel face and measurement reference is incomplete. Different knife systems can use different geometry.
Should I sharpen or replace my chipper knives?
Have their condition and remaining geometry assessed against the applicable service limits. Record the proposed finished dimensions before authorizing work. Suspected cracks or mounting damage require a technical disposition; a sharper edge does not resolve those defects.
Can I install one new knife beside previously sharpened knives?
Obtain the machine’s group, geometry and balance requirements before deciding. Record the condition of the retained knives. The approved arrangement determines whether individual replacement or a larger matched group is required.
How long should replacement chipper knives last?
There is no reliable interval without a defined duty and acceptance basis. Record feed, contamination, service history and the reason for removal. Compare service periods under sufficiently similar conditions before using life claims in a purchasing decision.
What if I have an old knife but no drawing?
Send both-face and side photographs, current measured dimensions with units, machine details and known sharpening or modification history. Agree on the original geometry and approve a drawing before manufacturing. The old sample remains evidence of its present condition.
Send a complete chipper-knife enquiry
Send NJDETE the machine manufacturer, model, serial number, part number, drawing revision and quantity for each knife position. Add L × W × T with units, mounting details, bevel and seating views, feed description and the reason for replacement. Identify any used samples, retained knives and unresolved requirements.
Ask for confirmation of the drawing, material, matched-group scope, inspection evidence and supply exclusions before production. Contact NJDETE about wood chipper blades to start the review, or browse the custom industrial blade range.
How this guide was prepared
This guide combines NJDETE’s published product scope with general knife-identification, purchasing and recordkeeping principles. It provides an enquiry framework, not a model-specific setup sheet. Illustrations are explanatory. No customer replacement results, part-specific test data or service-life figures are asserted here.