

Factory Acceptance Test for Industrial Shredders
Release time: 2026-10-24
Agree the test plan while the order is still being defined. If “capacity” means input fed into the hopper to one party and usable output collected over an elapsed hour to the other, the dispute starts before the machine runs.
Send NJDETE your material and acceptance requirements before finalising the configuration. Include feed photographs, largest and thickest items, required accepted output and the downstream process.
Define Which Test You Are Buying
A useful factory acceptance test procedure states its purpose and limits. The same run may support several decisions, but the report should distinguish them.
| Activity | Main question | Limit of the evidence |
|---|---|---|
| Demonstration | Can this machine engage and reduce the shown feed? | Does not establish the full feed range, sustained output or delivered configuration |
| Application trial | Which cutting system and preparation suit the material? | May use a development or demonstration machine rather than the ordered unit |
| Factory acceptance test, FAT | Does the identified ordered build meet the agreed factory checks? | Establishes results under the recorded test conditions and scope |
| Site acceptance test, SAT | Does the installed equipment meet the agreed site checks? | Depends on actual utilities, installation, integration and site feed conditions |
This is a procurement framework. The order must define the required checks, responsibilities and applicable obligations for the destination and application. Calling a demonstration an FAT does not add missing evidence, and an FAT is not a substitute for checks that depend on the installed site.
The distinction matters for commercial decisions. State which results support final configuration approval, which support shipment release, and which remain subject to site verification.
Identify the Exact Machine Before the Run
Record the order number, unit identification, approved configuration revision, motor and reducer, cutter arrangement, controls and included handling equipment. If the test uses a different unit, identify the differences and agree what can legitimately be transferred to the ordered build.
NJDETE’s published 500-model pages illustrate why the model number is insufficient:
| Published NJDETE configuration | Listed motor | Listed reducer | Listed chamber |
|---|---|---|---|
| 500 model with K97 | 7.5 kW | K97 | 500 × 400 mm |
| 500 model with ZQ400 | 11 kW × 1 | ZQ400 | 500 × 400 mm |
These are published configuration references, not tested capacity figures. The same chamber dimensions do not establish equal output. A higher motor rating alone does not establish cutter-shaft torque, duty capability or the material that can be processed.
Use the signed order and approved configuration for acceptance. Do not combine a catalogue model, a different product page and a trial video’s specifications into one assumed machine.
Build the Factory Acceptance Test Checklist
For each requirement, record the method, target or limit, evidence and decision owner. “Runs well” cannot be checked consistently by two reviewers.
| Requirement | Agree before testing | Record during or after testing |
|---|---|---|
| Machine identity | Ordered build and permitted deviations | Unit identification, configuration revision and difference list |
| Feed | Material, form, preparation, contaminants permitted and excluded | Batch identification, photographs, measured input and actual preparation |
| Capacity | Accepted-output definition, time boundary and required result | Weights, timestamps, interruptions and calculated rate |
| Output quality | Downstream requirement, sample method and reject classification | Samples, method, results and rejected quantity |
| Functions | Approved functional-check procedure and responsible personnel | Check result, observed fault and evidence reference |
| Utilities and energy | Supply conditions and equipment inside the metering boundary | Actual supply, meter readings and included auxiliaries |
| Deliverables | Required drawings, manuals, records, spares and packing scope | Received revision, missing item and responsible person |
| Disposition | Who can accept, hold or authorise a conditional release | Signed decision, conditions, action owner and retest requirement |
Choose batch size, run duration and repetitions around the intended duty and variability. There is no single sample weight or demonstration length that validates every shredder application. A short run may identify a feeding problem while saying little about sustained production.
For sizing assumptions before acceptance planning, use the Guía de capacidad de trituradoras industriales. The FAT report should then record how the agreed requirement was measured on the identified build.
Prepare a Representative and Traceable Batch
Send material that represents normal supply, including the difficult forms within the agreed feed specification. A batch of loose, clean offcuts cannot validate a stream that normally arrives nested, strapped or heavily compacted.
Record material type, source, largest dimensions, thickest section, packaging or nesting, moisture condition where relevant, and any preparation. Record the amount removed before testing and why. If the machine receives pre-cut pieces, report the preparation labour and equipment separately instead of presenting the result as whole-item processing.
Agree excluded or unapproved material before dispatching the trial batch. Unexpected items should become a documented deviation, rather than an improvised test of the machine’s limits.
Identify the weighing equipment, suitable measurement resolution and relevant verification record. Tare containers and identify the collection points. Record the machine’s starting condition so output or residue from an earlier run is not counted as production from the test batch.
Reconcile the Material and Measure Usable Output
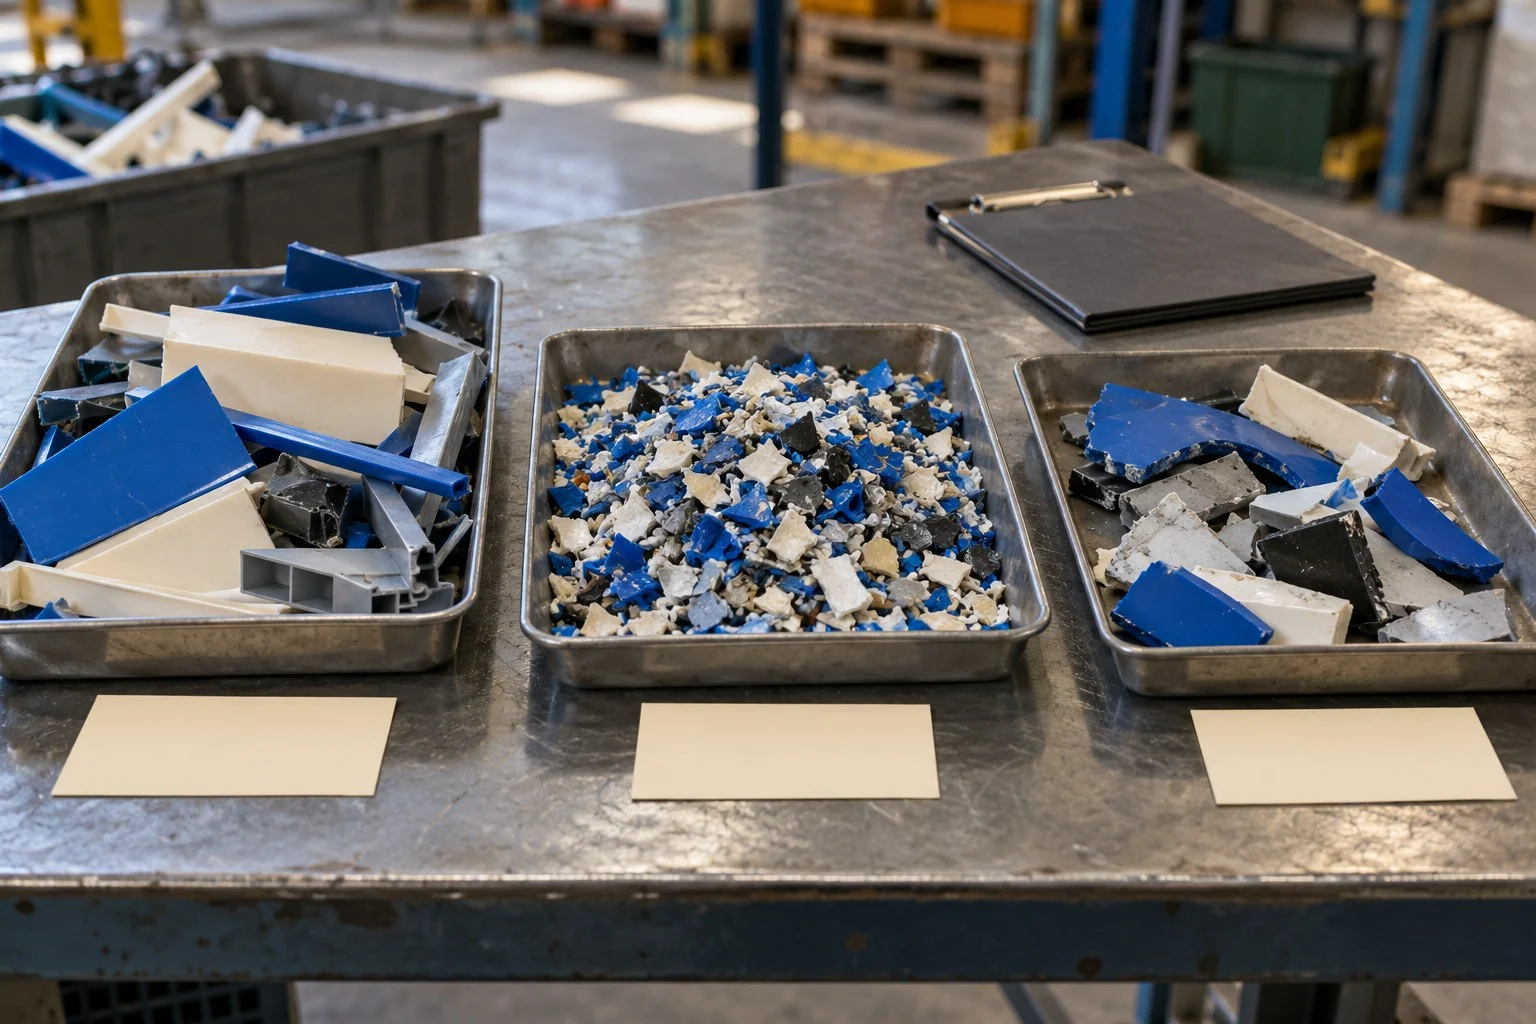
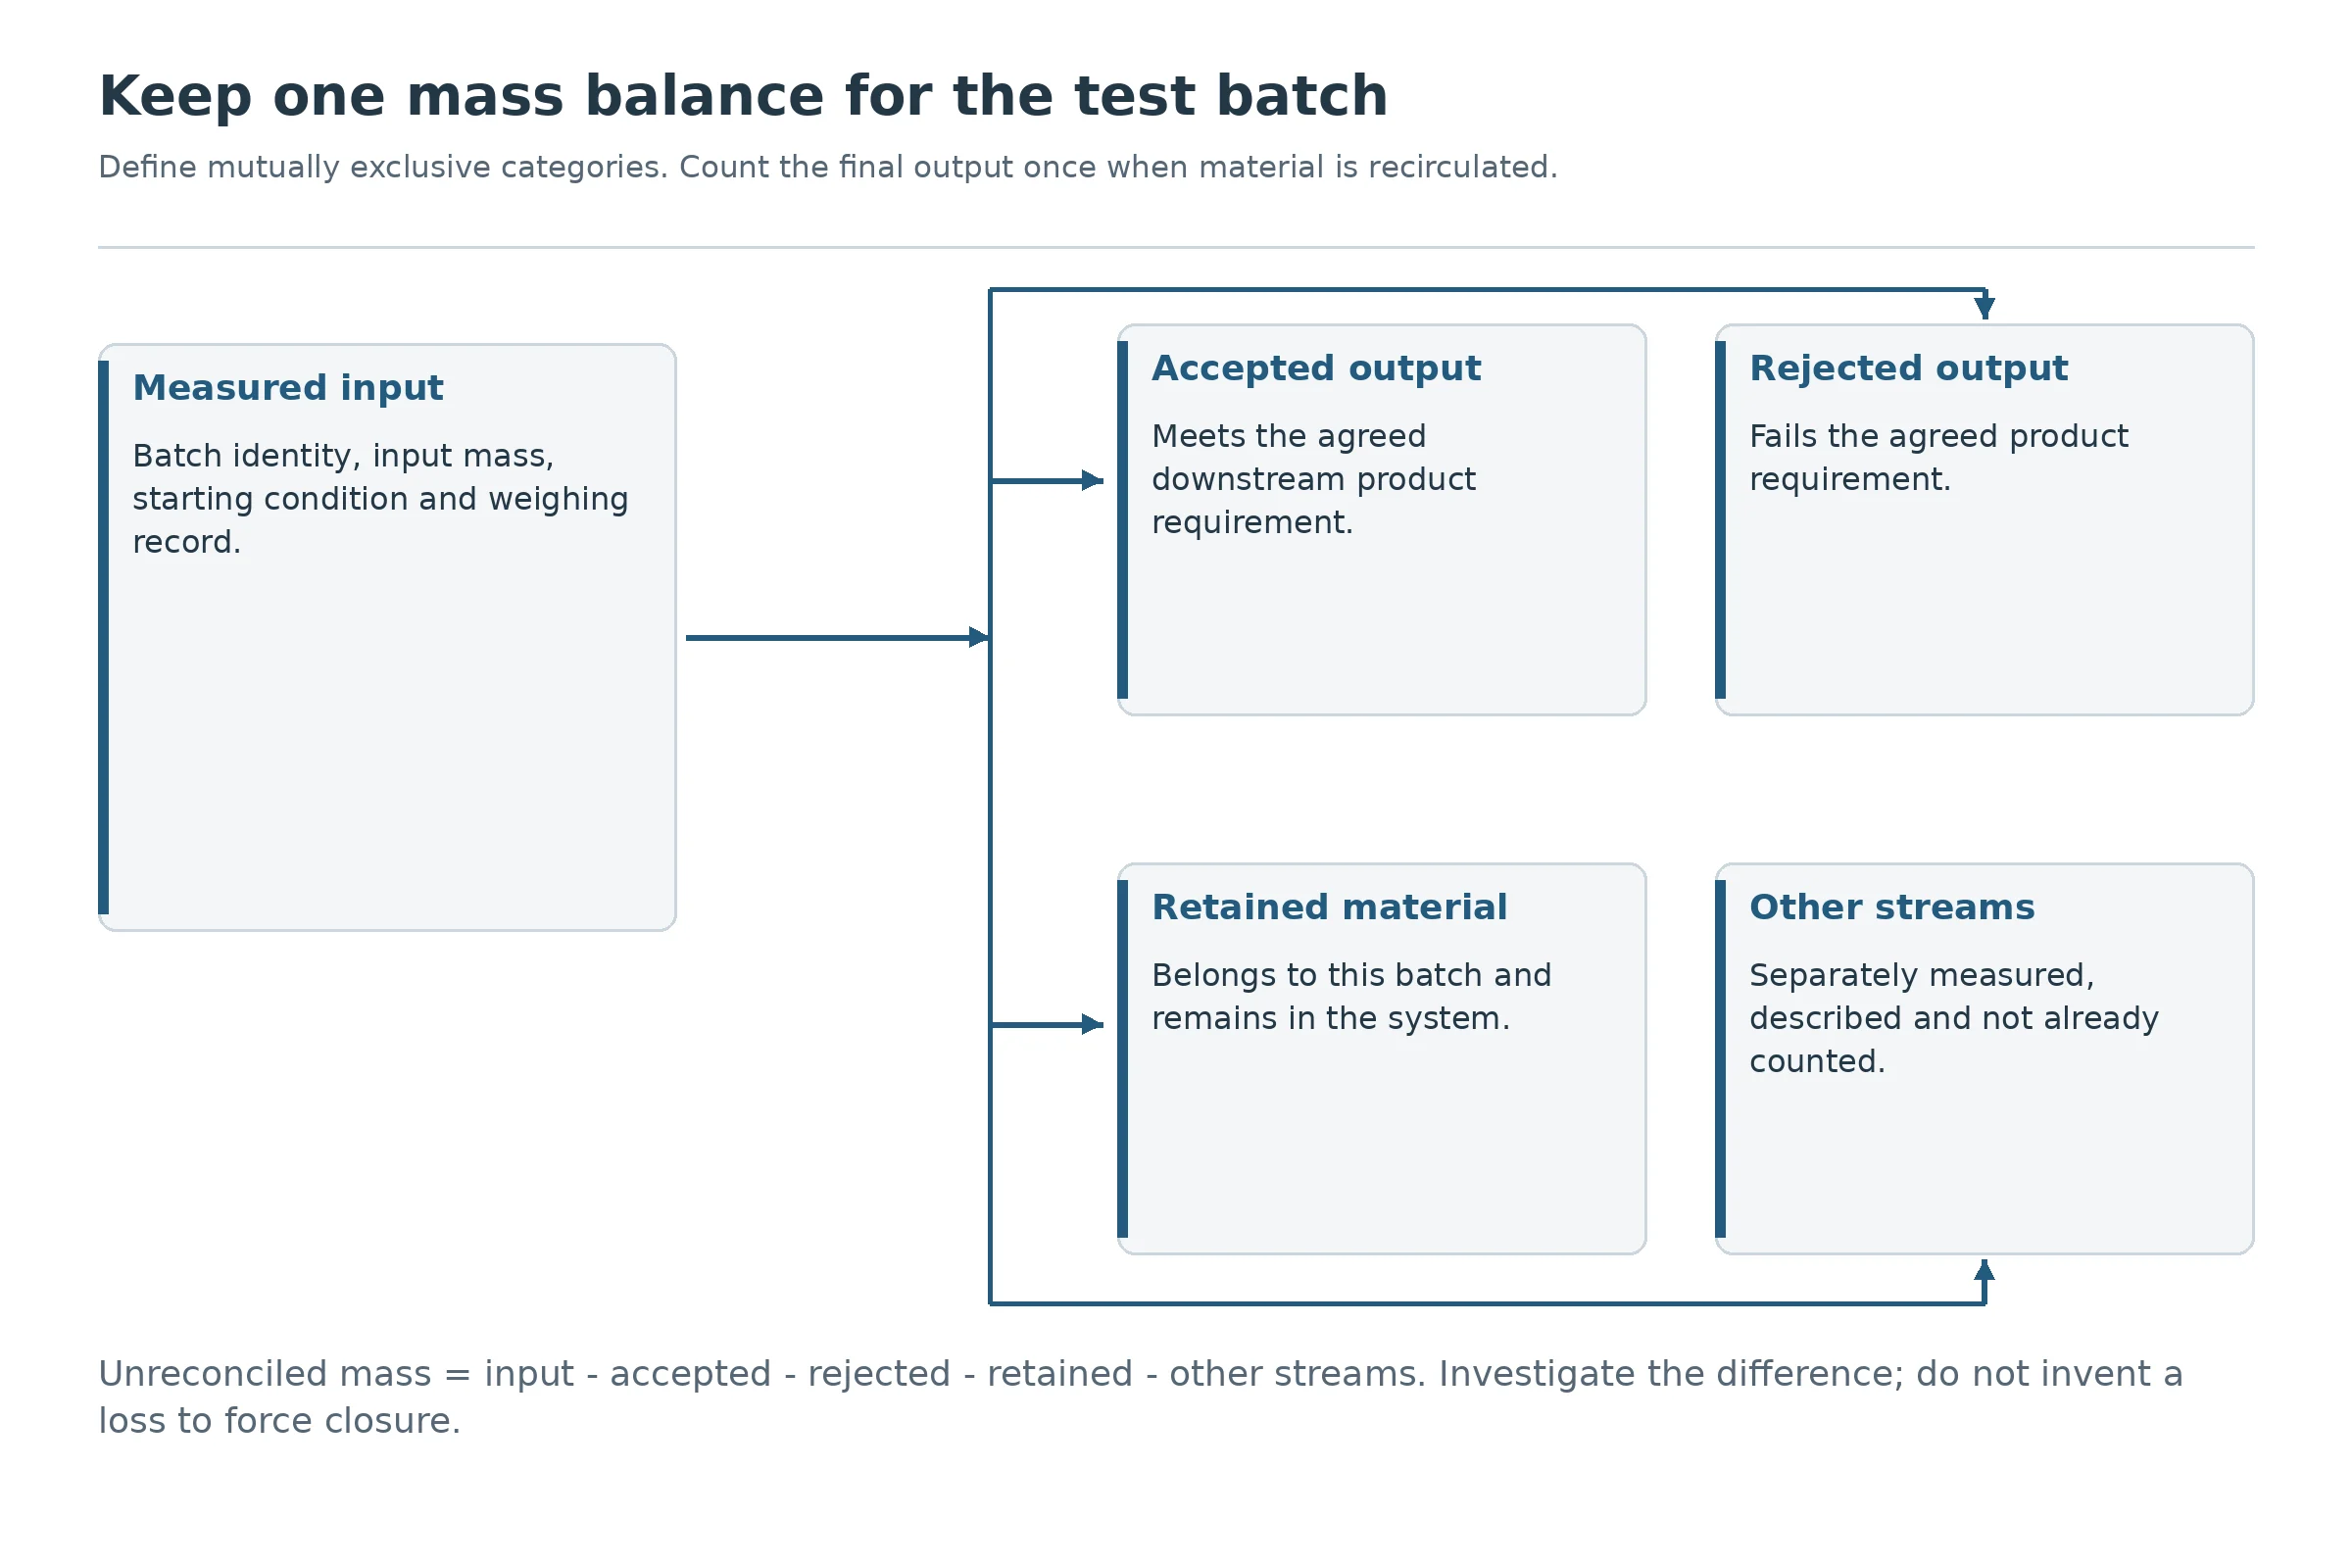
Input mass is not automatically accepted output. Separate usable product, rejected product, material remaining in the system and other collected streams. Define the categories so the same kilogram cannot appear twice.
Unreconciled mass = input mass − accepted output − rejected output − retained material − other separately recorded streams.
An “other” stream needs a description, such as separately collected fines. Investigate a difference using the actual collection and measurement conditions. Moisture change, residue, collection loss or weighing error may affect closure. Do not enter an invented loss figure simply to force the balance to zero.
If rejected pieces are recirculated, count final accepted material once. Additional passes add processing time; they do not create additional input mass from the same batch. Retained material is identified and recovered only through the machine’s approved procedure by authorised personnel.
Output size needs its own acceptance method. Agree the sampling locations and timing, sample amount, measurement method and treatment of oversize. A blade thickness, a screen opening or one attractive sample photograph is not a complete description of the whole output distribution. Long strips and irregular pieces can matter to the next process even when their narrow dimension looks acceptable.
Keep the sample identifier with the batch and machine record. Where washing, granulation, separation or conveying follows the shredder, define what that next stage can actually accept.
Use an Explicit Time and Energy Boundary
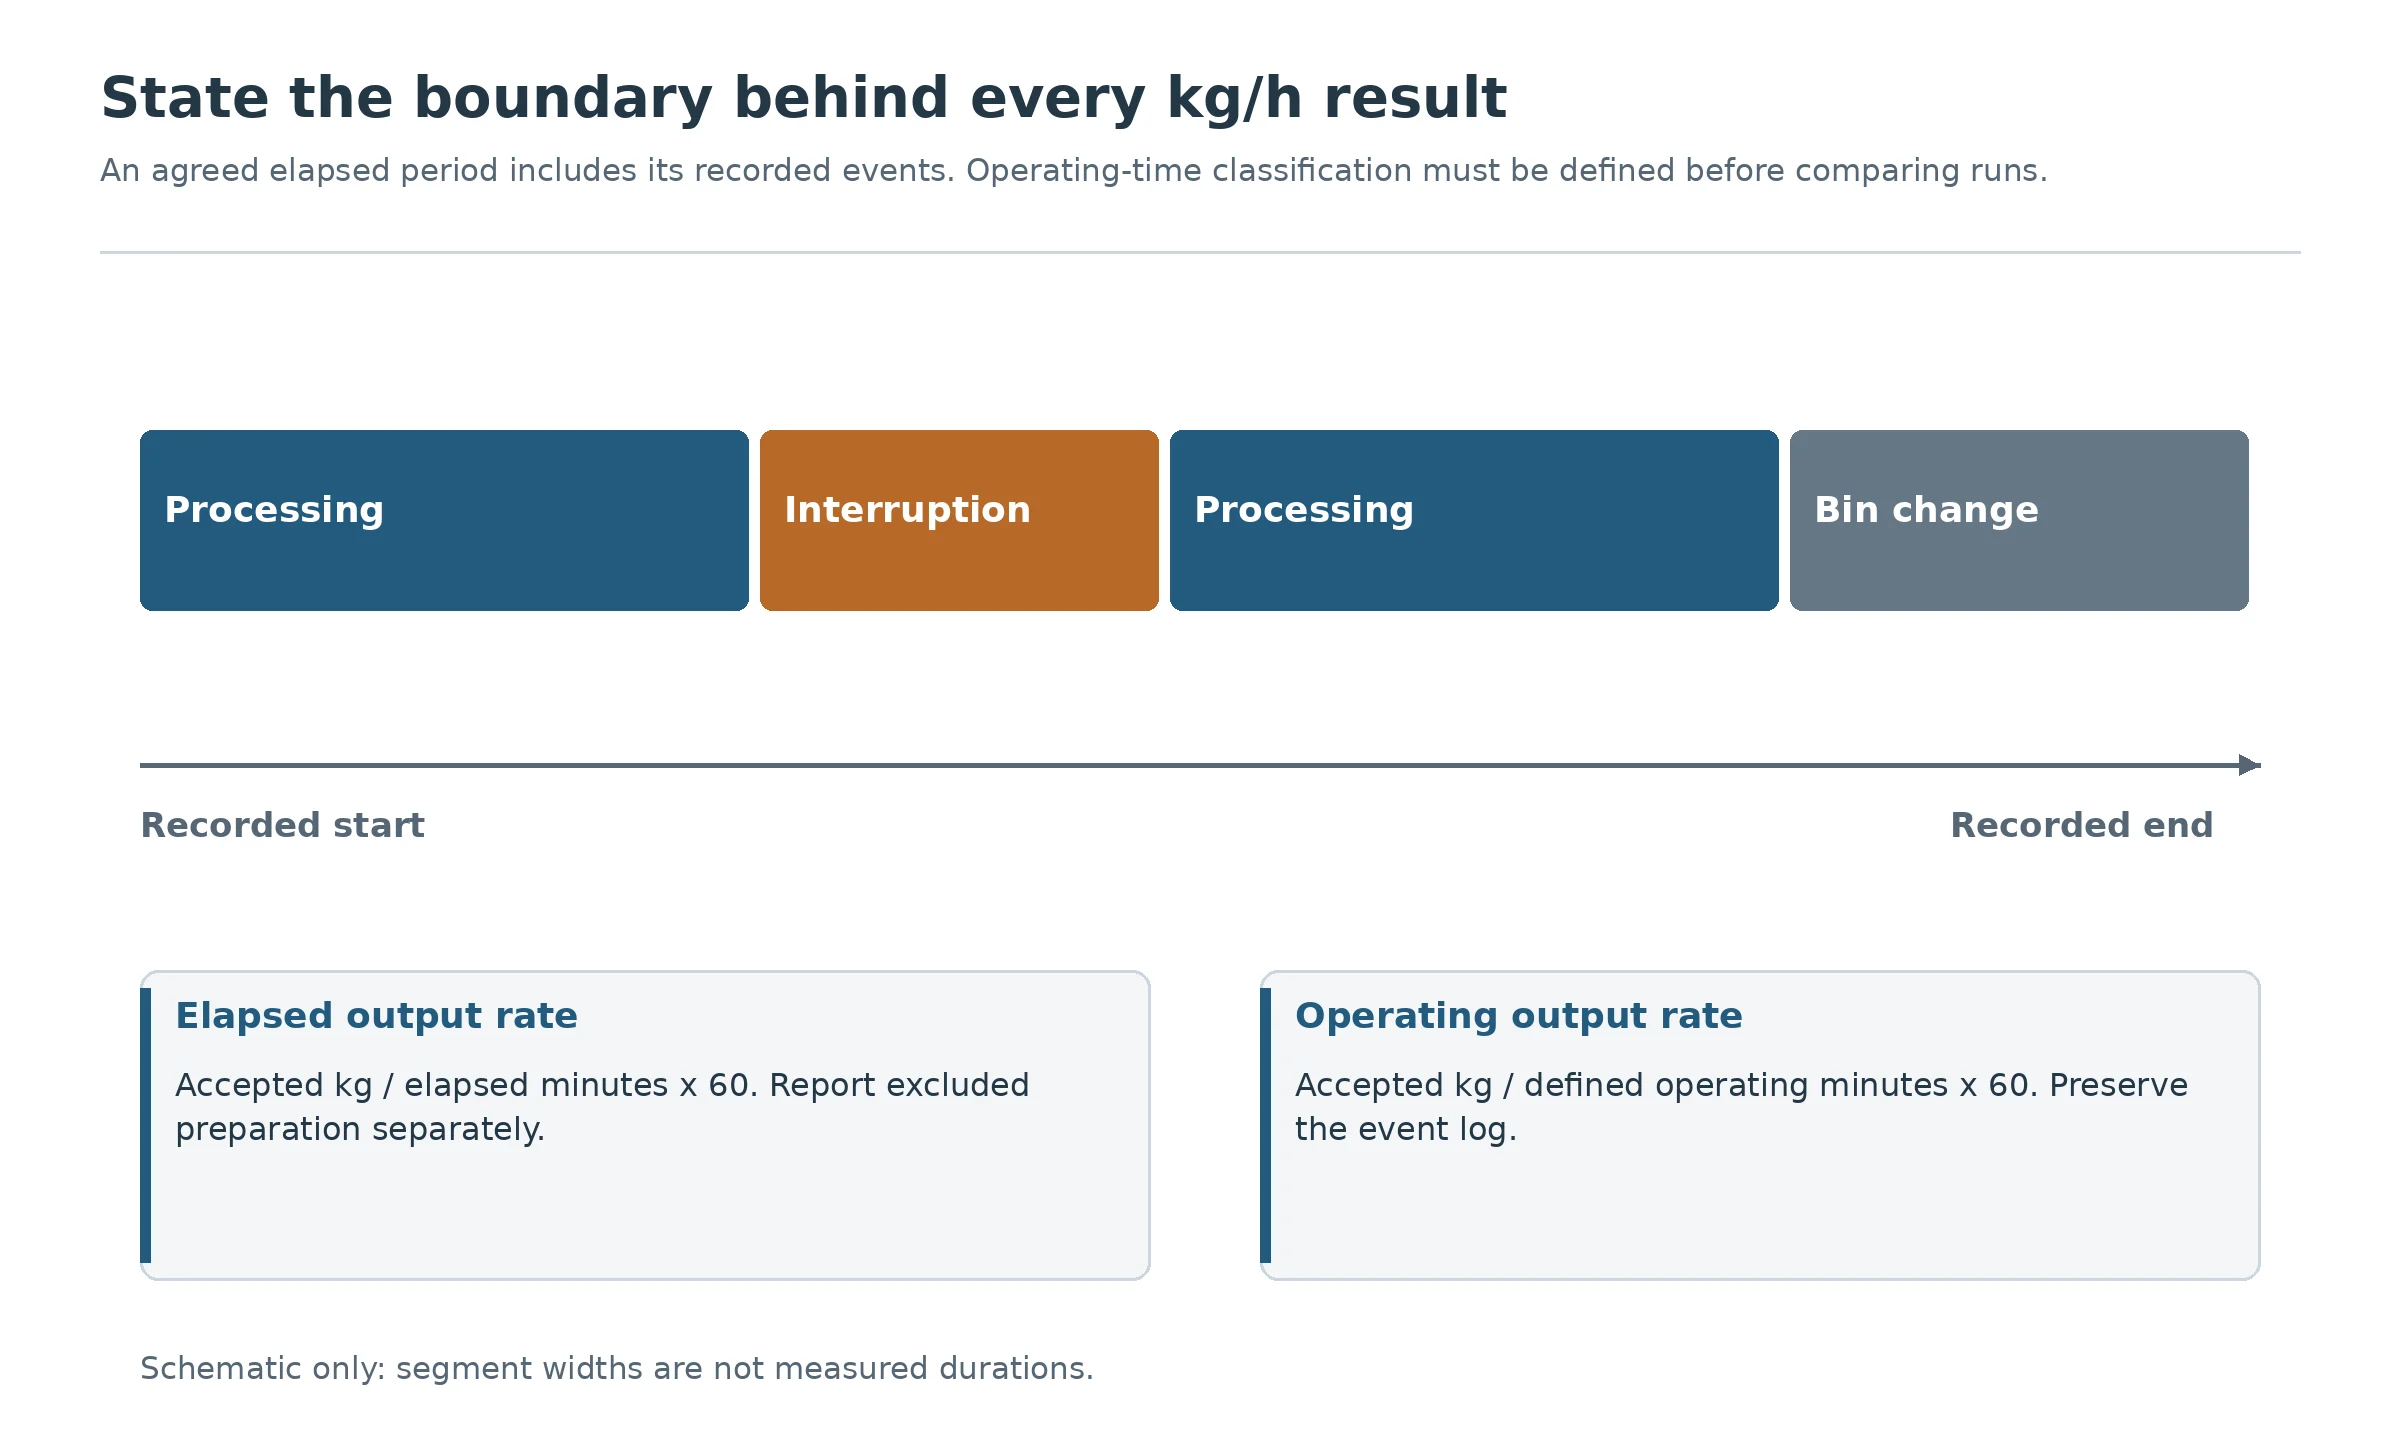
Record both the agreed elapsed period and the defined operating time. List included pauses, reversals, refilling, bin changes and downstream interruptions. State how operating time is classified; it should not quietly change between runs.
Accepted output per elapsed hour = accepted output in kg ÷ elapsed minutes × 60.
Accepted output per operating hour = accepted output in kg ÷ defined operating minutes × 60.
The operating figure can help examine the cutting process. The elapsed figure exposes interruptions within the agreed production boundary. If preparation or cleaning sits outside that boundary, report it separately so the buyer can assess the complete production task.
Worked Calculation: Hypothetical Batch
The figures below explain the calculation. They are not an NJDETE capacity test, customer case or promised result.
| Recorded item | Hypothetical value |
|---|---|
| Input | 300 kg |
| Resultado aceptado | 270 kg |
| Rejected output | 12 kg |
| Retained material | 15 kg |
| Other collected stream | 2 kg |
| Elapsed period | 60 minutes |
| Defined operating time within that period | 45 minutos |
| Energy measured over the same period and agreed equipment boundary | 7.2 kWh |
This record gives 270 kg/h on elapsed time, 360 kg/h on operating time, and 90% accepted mass yield. The unreconciled difference is 1 kg, approximately 0.33% of input. Whether that difference is acceptable depends on the agreed measurement method and tolerance; it should not be silently erased.
Specific energy on accepted output is 7.2 ÷ (270 ÷ 1,000) = approximately 26.7 kWh/t. It is meaningful only with the metered equipment and period stated. Motor nameplate power is not measured energy consumption. A meter covering the shredder alone cannot establish the consumption of a complete line with conveyors, extraction and downstream equipment.
Record Functions, Deviations and Retests
Qualified personnel should carry out the agreed functional checks using the machine’s approved test procedure. Identify the checked functions, expected response and evidence. Do not improvise faults, bypass protective functions or substitute an article checklist for the manufacturer’s procedure.
Give every deviation a reference number. Record the requirement, observation, effect, proposed correction, responsible person, due date and evidence required to close it. A second run should identify what changed and which checks were repeated.
| Disposition | What the record needs to show |
|---|---|
| Accepted | The agreed scope and criteria were met, with the required evidence |
| Hold for correction or retest | Open requirement, corrective action and checks needed before reconsideration |
| Conditional release, if expressly agreed | Exact open items, limitations, responsibility, completion evidence and authorised decision |
A capacity result alone does not close an unresolved output-quality, protective-function or documentation requirement. Nor does “conditional” mean the machine has passed all checks. The buyer and supplier need an explicit disposition for each open item and for shipment.
If the difficulty is repeated reversal, jamming or interrupted discharge, retain the event sequence rather than reporting only the final average. The shredder troubleshooting guide explains what observations help a technical review.
What Belongs in the Factory Acceptance Test Report?
Keep the approved plan, configuration, material record, measurements, output samples, function checks, deviations and final disposition together. Include dates, responsible people, instrument identification and the revisions of relevant documents. Reviewers should be able to reproduce the reported rate from the recorded weights and times.
Photographs and video should identify the actual run and support the written record. A continuous view may help explain feeding and interruptions, but video cannot replace the weighing, time or acceptance criteria that it does not show.
The following NJDETE channel video is a cardboard-shredding demonstration. It provides an application view; it is not the FAT report for your order and establishes no measured throughput here.
Watch the NJDETE cardboard shredding demonstration on YouTube.
Reserve site-dependent checks for the agreed SAT or commissioning scope: installed utilities, actual feed and discharge integration, site access, and production conditions that were not reproduced at the factory. The FAT report should identify these outstanding boundaries rather than imply they were tested.
Preguntas frecuentes
Is a factory acceptance test the same as a demonstration?
No. An FAT checks an identified ordered build against an agreed plan and criteria. A demonstration can show material engagement, but may omit measured output, configuration identity, functional checks and a written acceptance decision.
How long should a shredder FAT run?
Long enough to address the agreed duty, feed variability and measurement requirements. The parties should set duration, batch size and repetitions in advance. A short successful run does not establish sustained performance under every production condition.
Should capacity use input weight or accepted-output weight?
Specify both where useful, but state which determines acceptance. Accepted-output rate connects the capacity result to the usable product requirement. Keep rejects, retained material, repeated passes and interruptions visible in the record.
What is the difference between FAT and SAT?
FAT covers the agreed factory checks before shipment. SAT covers the agreed checks after installation at the site. Actual utilities, integration and feed conditions can require site verification even when the factory checks are complete.
Can a remote FAT be accepted by video?
The parties can agree remote witnessing, but the evidence requirements remain. Identify the unit, instruments, batch, timestamps, output and deviations, and agree how witnesses review and sign the record. A short edited clip alone leaves many of these items unresolved.
Does meeting the kg/h target mean the machine has passed?
Only if all the other agreed requirements are also satisfied or explicitly dispositioned by authorised parties. Throughput does not, by itself, establish output quality, required functions, documentation completeness or site suitability.
Prepare the Trial Brief with NJDETE
Send the feed description and photographs, expected material variation, largest and thickest sections, preparation permitted, accepted-output target, downstream requirement, site power supply and intended working schedule. Add witnessing preferences and the documents required with the order.
Ask the quotation to identify the configuration, proposed material trial, acceptance measurement method and checks left for site installation. For the wider purchasing review, use industrial shredder supplier evaluation.
Contact NJDETE to define the configuration and trial brief. Put the feed, accepted product, measurement period and decision criteria into the order so the test answers a production question you can verify.